

What faults do spray dryers encounter and solutions
Views: 0 PublishTime: 2026-09-17
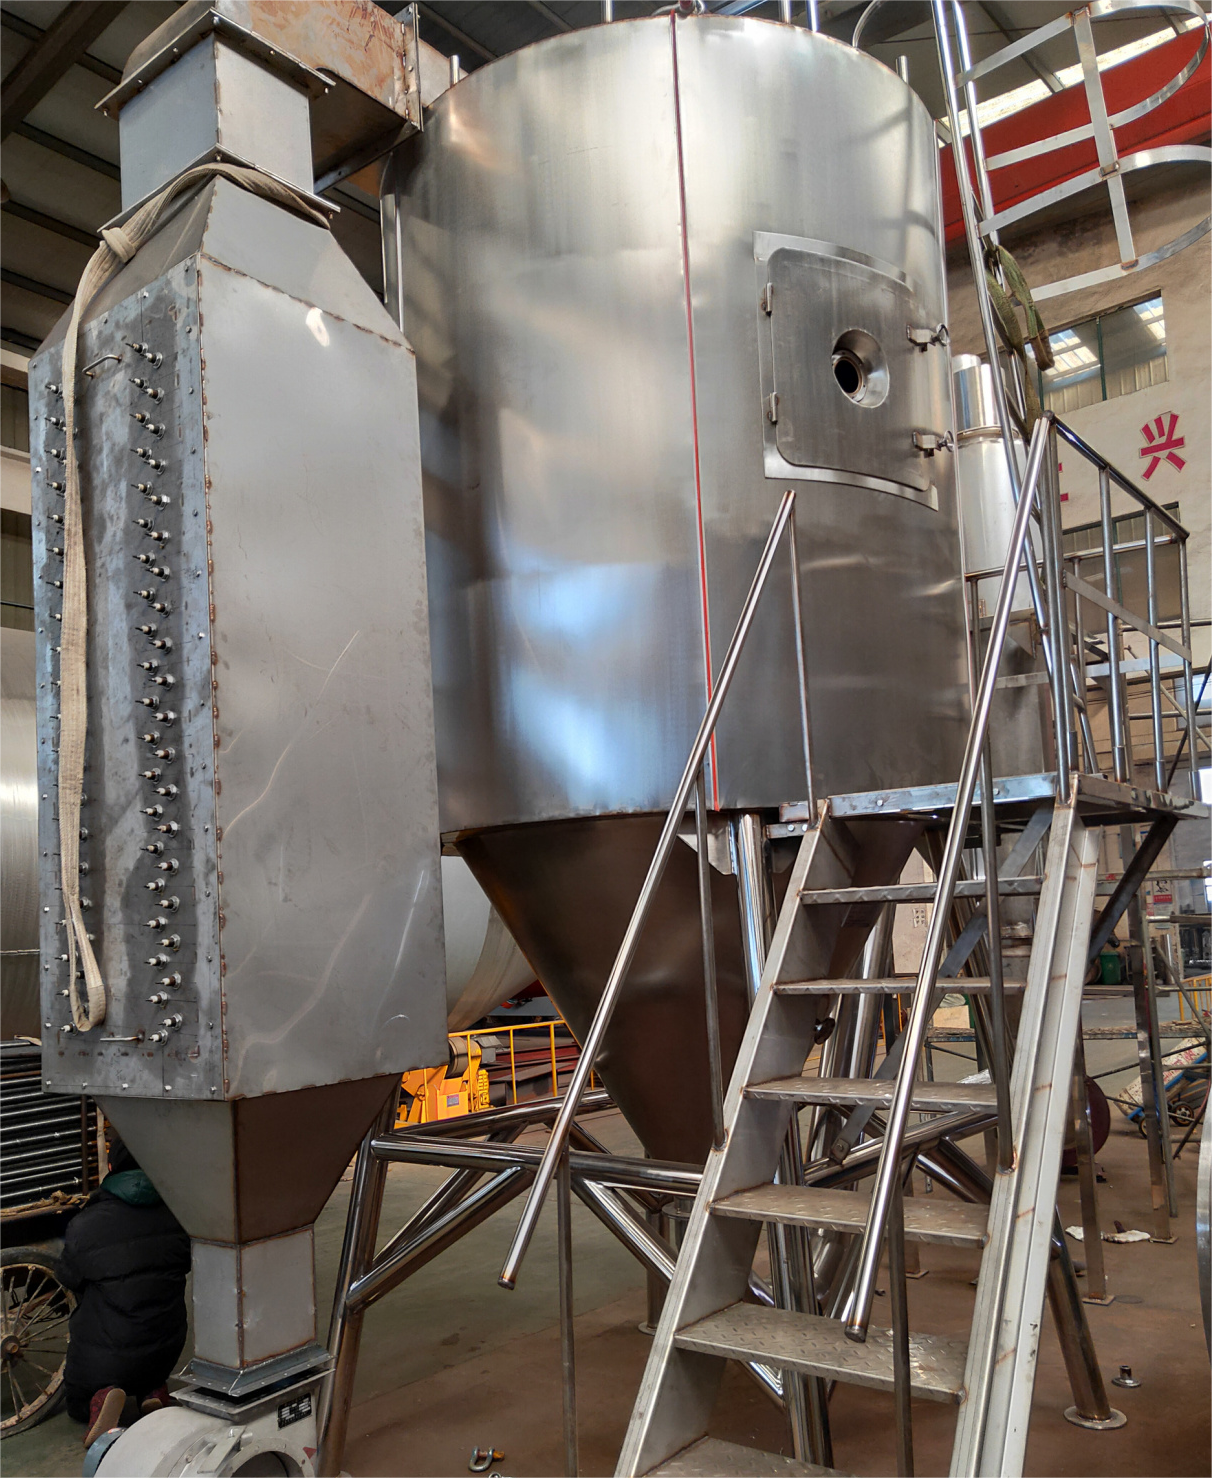
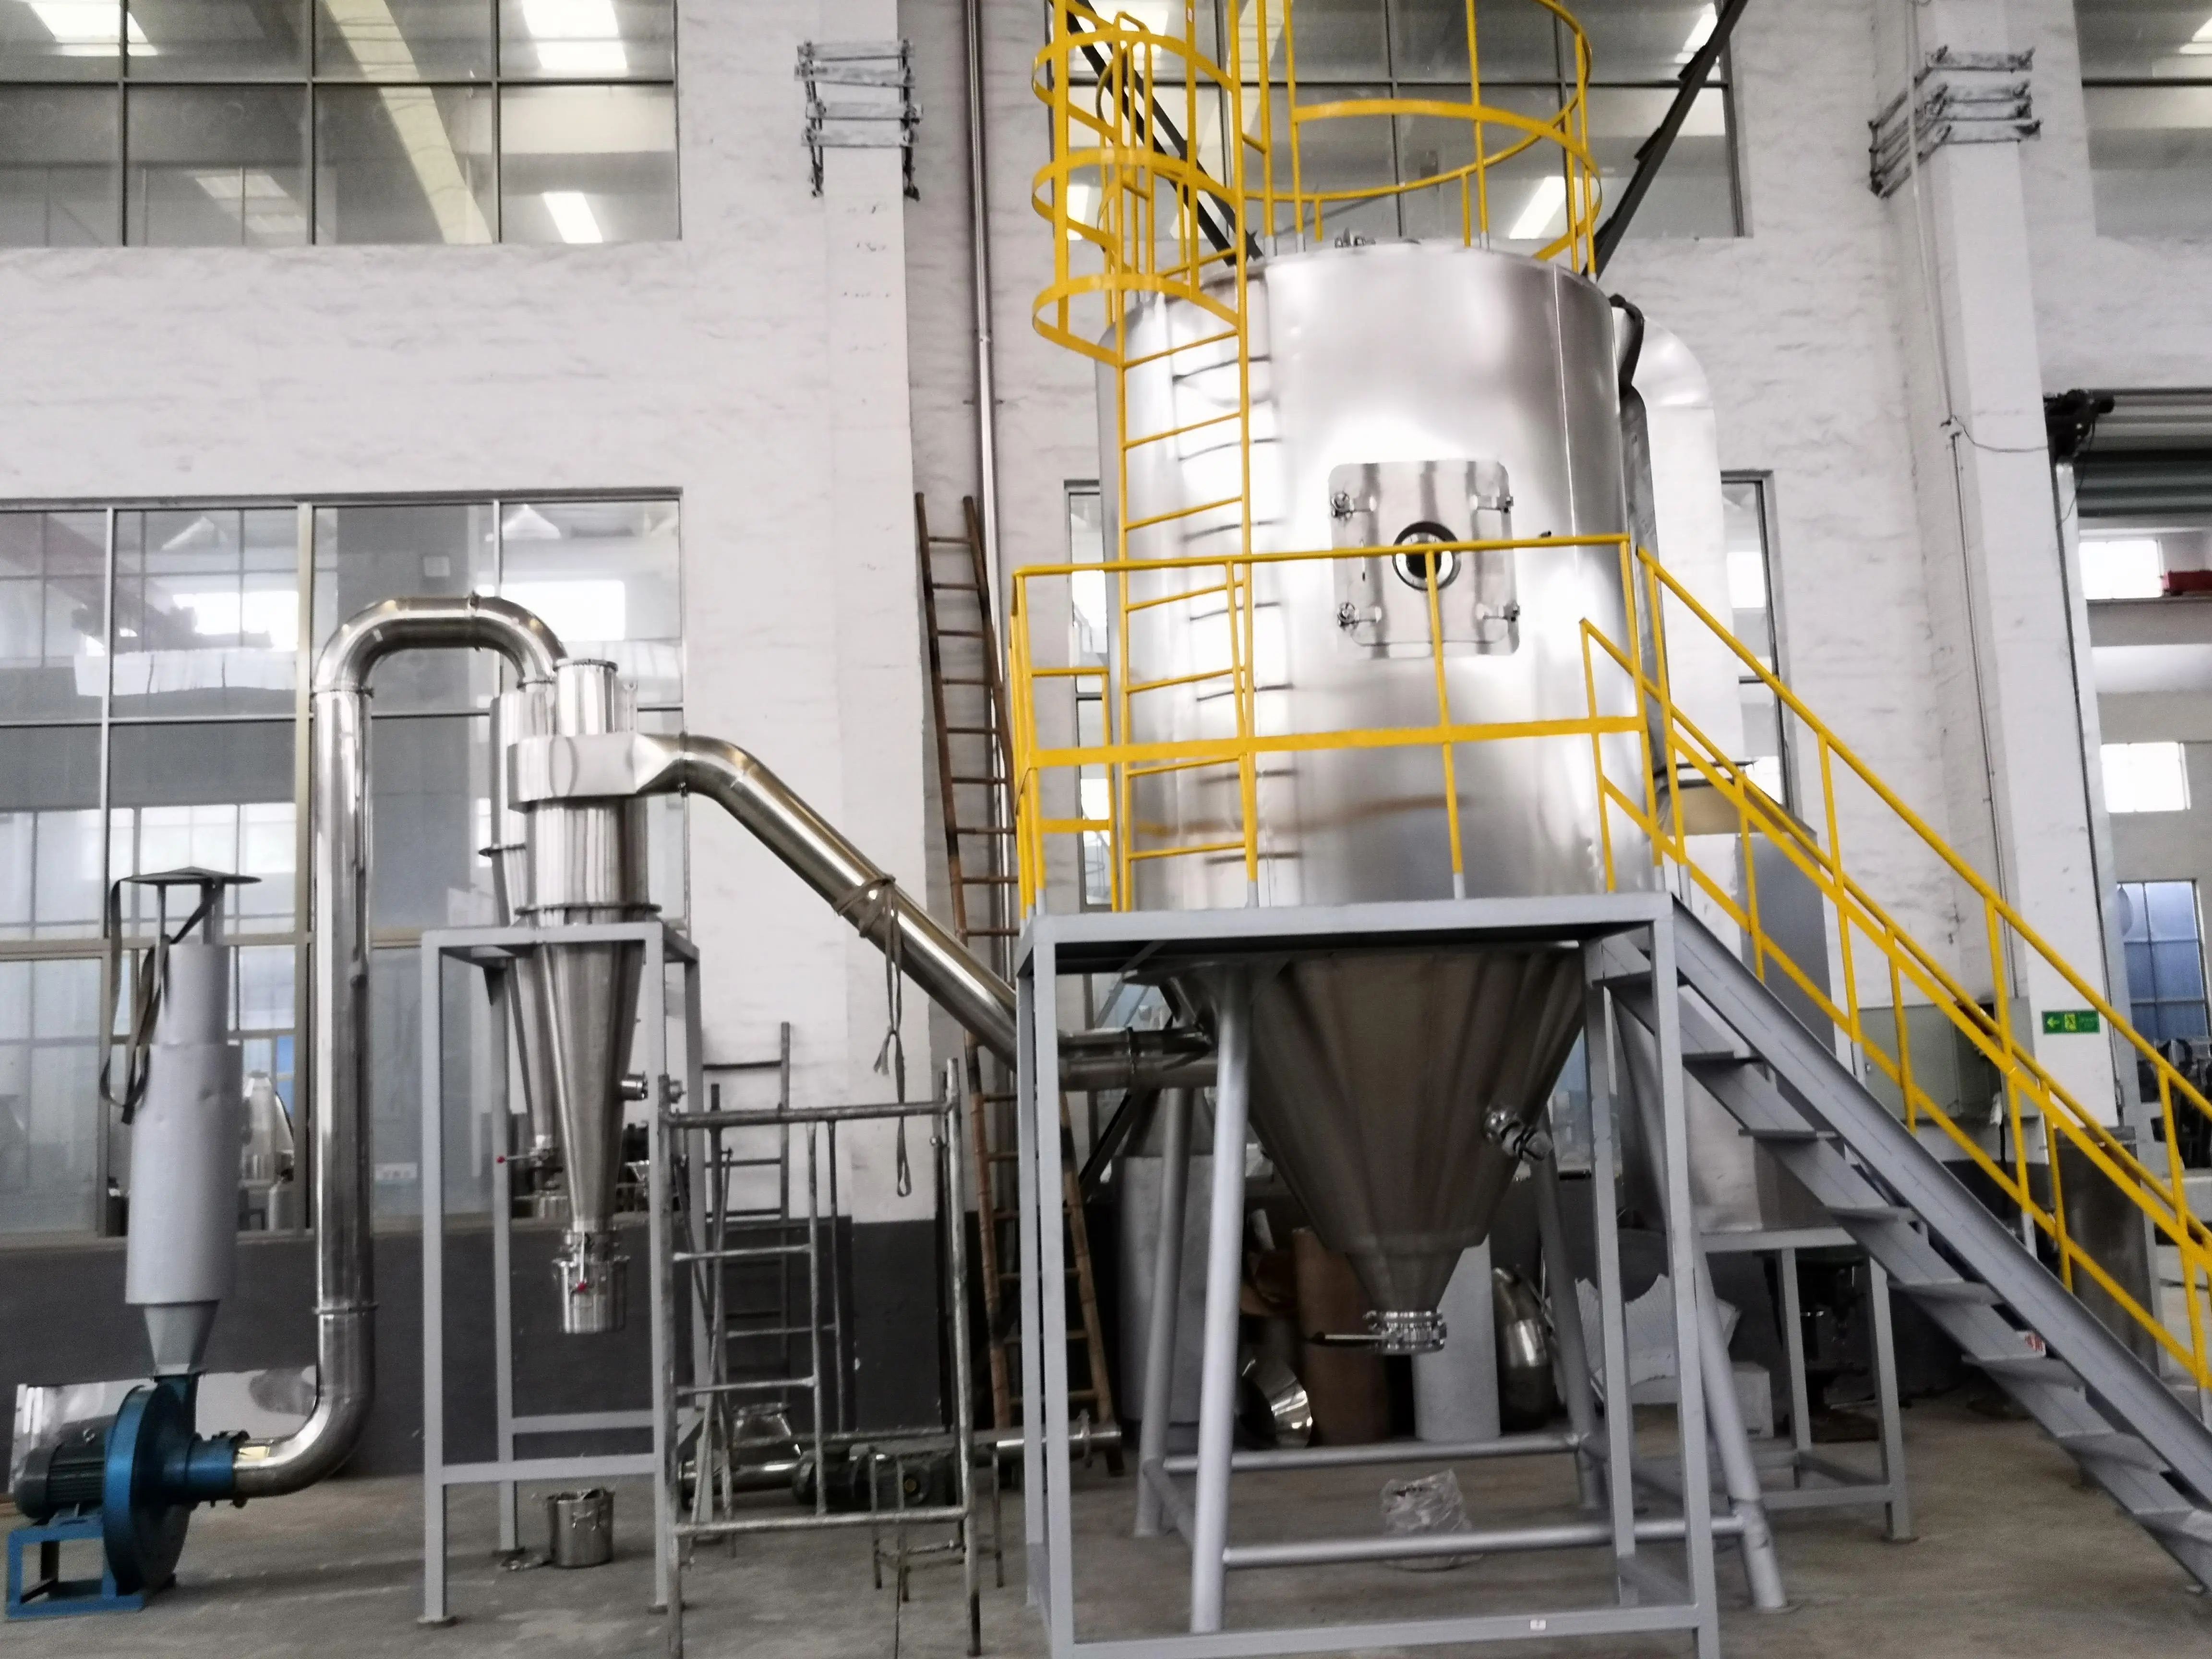
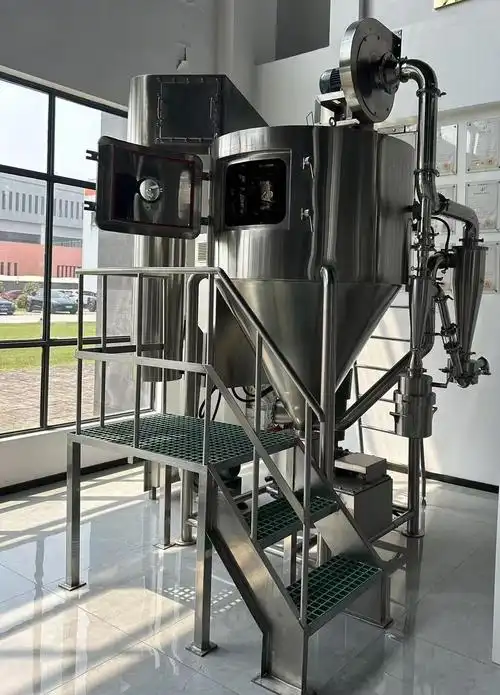
During the operation of the spray dryer, common faults focus on poor drying effect, sticky discharge wall, blocked pipe rows, abnormal atomization and mechanical noise. The following are common failure causes and solutions:
1. Solve the problem that the water content of the discharge is too high (incomplete drying):
Core inspection: inlet/outlet air temperature and feed volume.
Reason: The exhaust air temperature is too low, the feeding speed is too fast, the hot air volume is insufficient, or the accumulation rate exceeds the preset range.
Exclusion method:
1. Properly reduce the feed pump to reduce the feed volume.
2. Increase the inlet air temperature or increase the hot air flow.
3. Check whether the filter is working normally and remove the sludge on the filter.
Verification method: Observe the sample at the discharge port, make it feel dry, and measure the moisture content to reach the set index.
2. Solve the problem of wall sticking in the tower (agglomeration/coking):
Core inspection: feed amount, atomization status and tower wall temperature.
Reason: Uneven spraying and atomization, too large feed amount, causing the wet materials to contact the tower wall, and the local temperature of the tower wall is too high (causing the materials to melt/coke).
Exclusion method:
1. Material storage: Properly reduce the inlet air temperature, or introduce a tower wall cold air jacket device (cold wall system).
2. Poor atomization: Readjust the atomizer and check whether the nozzle is worn or eccentric.
3. The flow rate is too fast: Reduce the feed amount and increase the exhaust temperature.
Verification method: Inspect frequently or check the inner wall of the tower through the observation window, and there is no obvious accumulation or coking spray.
3. Solve atomizer abnormalities (dripping, clogging or severe vibration):
Core inspection: nozzle/centrifugal disk and bearing maintenance.
Reason:
Dripping/clogging: excessive accumulation, unfiltered, high feed clogging or nozzle clogging.
Closing/abnormal sound: unbalanced centrifugal atomizing disk, damaged bearing, bent rotation or poor lubrication.
Exclusion method:
1. Blockage: Clean the nozzle or centrifugal disk; add a filter screen to the feed pipe (recommended 80-100 mesh).
2. Shut down: Check whether the centrifugal disk is damaged and the dynamic balance is damaged, clean it up; if the bearing is worn, replace it in time; add lubricating oil.
Verification method: Start the atomizer idle and water test. The atomized water mist is evenly circular, and there is no abnormal bat collapse or noise.
4. Solve system powder leakage/low recovery rate:
Core inspection: cyclone separator and bag separator.
Causes: The cyclone separator is not tightly sealed (air leakage), the bag filter is damaged or blocked, and the air volume and pressure of the induced draft fan are not matched.
Exclusion method:
1. Check whether the air shutoff valve/collecting barrel sealing ring at the bottom of the cyclone separator is complete to ensure that there is no air leakage.
2. Check and clean the bag filter, and replace it in time.
3. Adjust the variable valve to maintain a micro negative pressure in the tower.
Verification method: Observe that there is no obvious overflow from the exhaust outlet, and the collection rate returns to the normal range.